Acceptance of a flying shear cut-to-length line should prove a complete production recipe, not only that each motor can run. Factory acceptance testing and site acceptance testing need agreed material, finished-sheet requirements, measurement methods and operating conditions so both parties judge the same result.
Define the test before the coil is loaded
Record the coil grade, thickness, width, weight, surface and identification, then confirm the blank length, quantity, target operating condition and applicable tolerances. The sample should represent real production; an easy coil or unusually long blank cannot validate a more demanding recipe. Instruments and reference surfaces must be suitable for the values being checked.
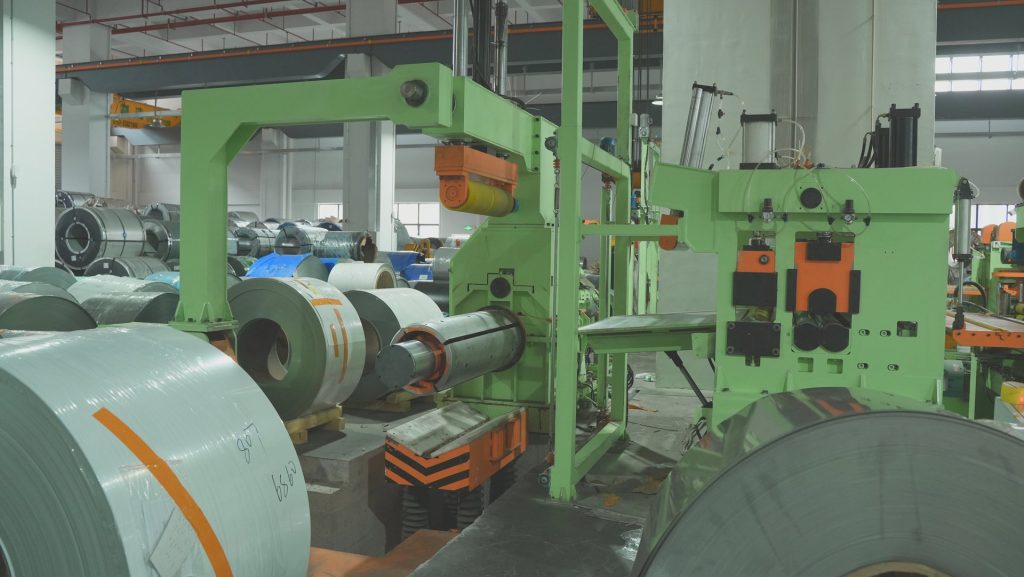
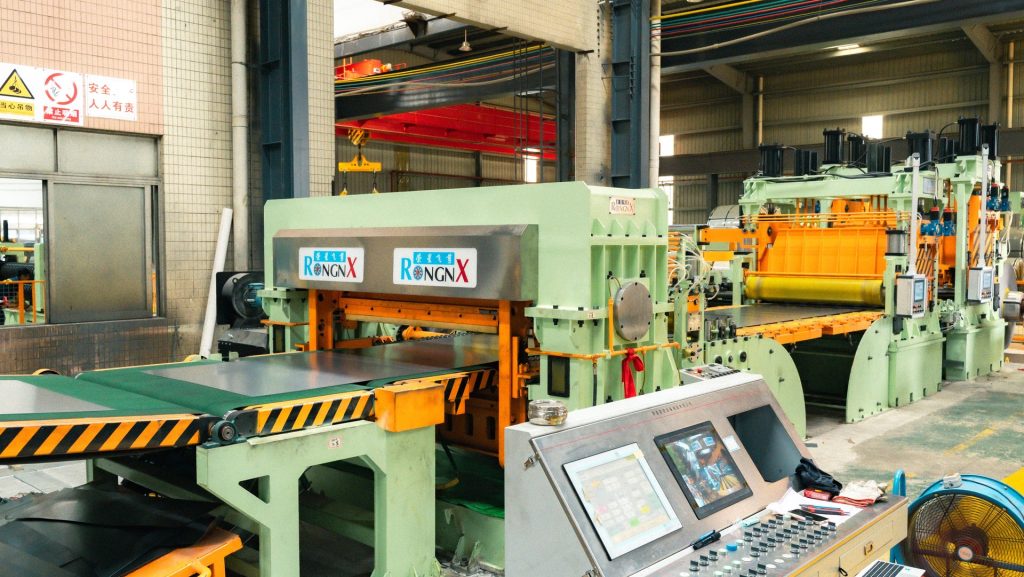
At the start of the run, verify loading, centering, expansion, payoff and safe threading. Follow the strip through guiding and leveling, then confirm that the measuring system and flying shear use the approved recipe. RONGXING’s 850mm customer-site acceptance case shows the value of evaluating the process from coil entry through protected stacking.
The protocol should also state who may change parameters during the trial and how each adjustment is recorded. Without that control, a successful final stack may not be tied to a repeatable setup that operators can restore later.
Measure output during sustained operation
Check more than the first sheet. Samples taken during a stable run should be identified and measured for length, diagonal, flatness and cut-edge condition against the agreed specification. Surface inspection should cover repeated marks, scratches and handling damage. Alarms, emergency stops, guarding and interlocks should be checked through the approved procedure without defeating safety functions.
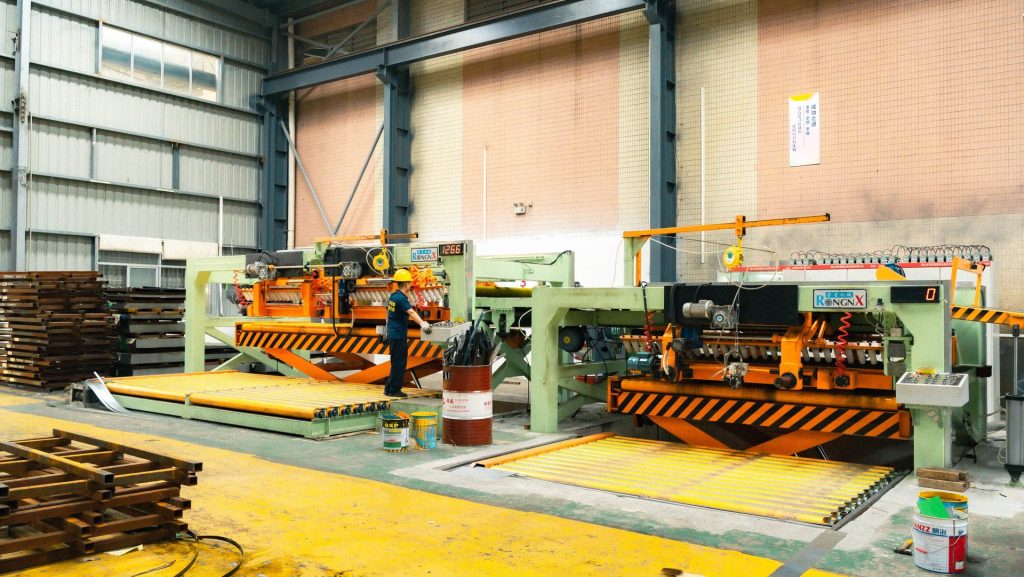
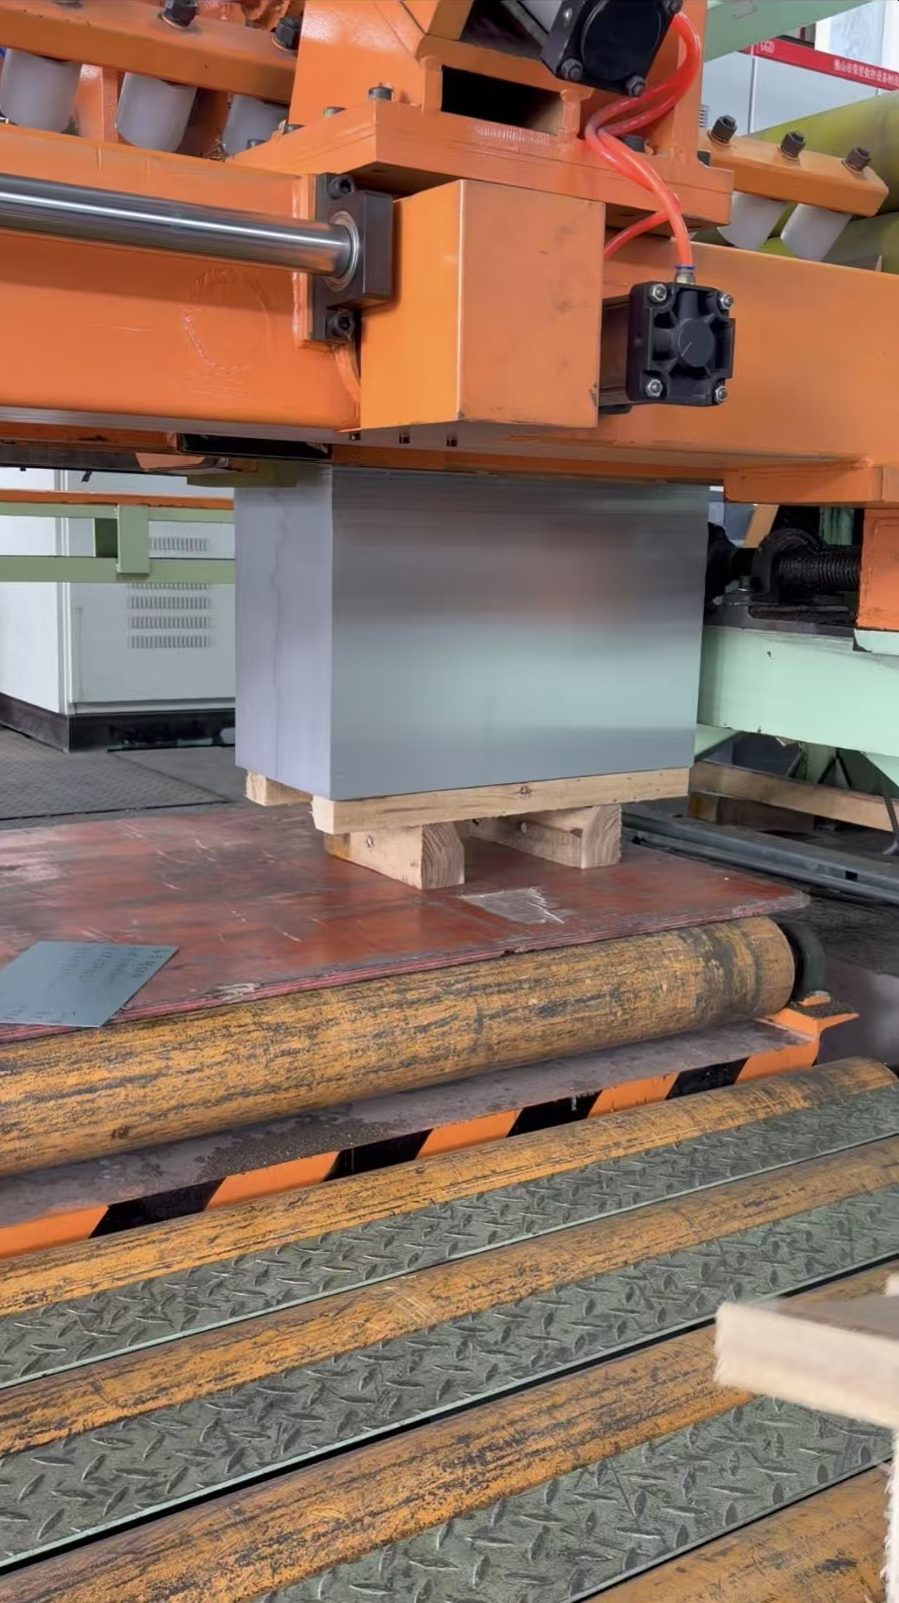
The discharge section must keep pace with cutting. Sheet separation, conveying, braking, side alignment, pile quality and bundle changeover all influence usable output. The comparison of single and dual stackers helps define which collection behavior belongs in the acceptance scope.
Close the test with records and open items
The final record should state the tested material and recipe, sample measurements, observed speed, stack condition, alarms and any agreed adjustments. Open items need an owner and closure condition. Operator training, lubrication points, wear parts, blade checks and recipe backup should also be documented before handover.
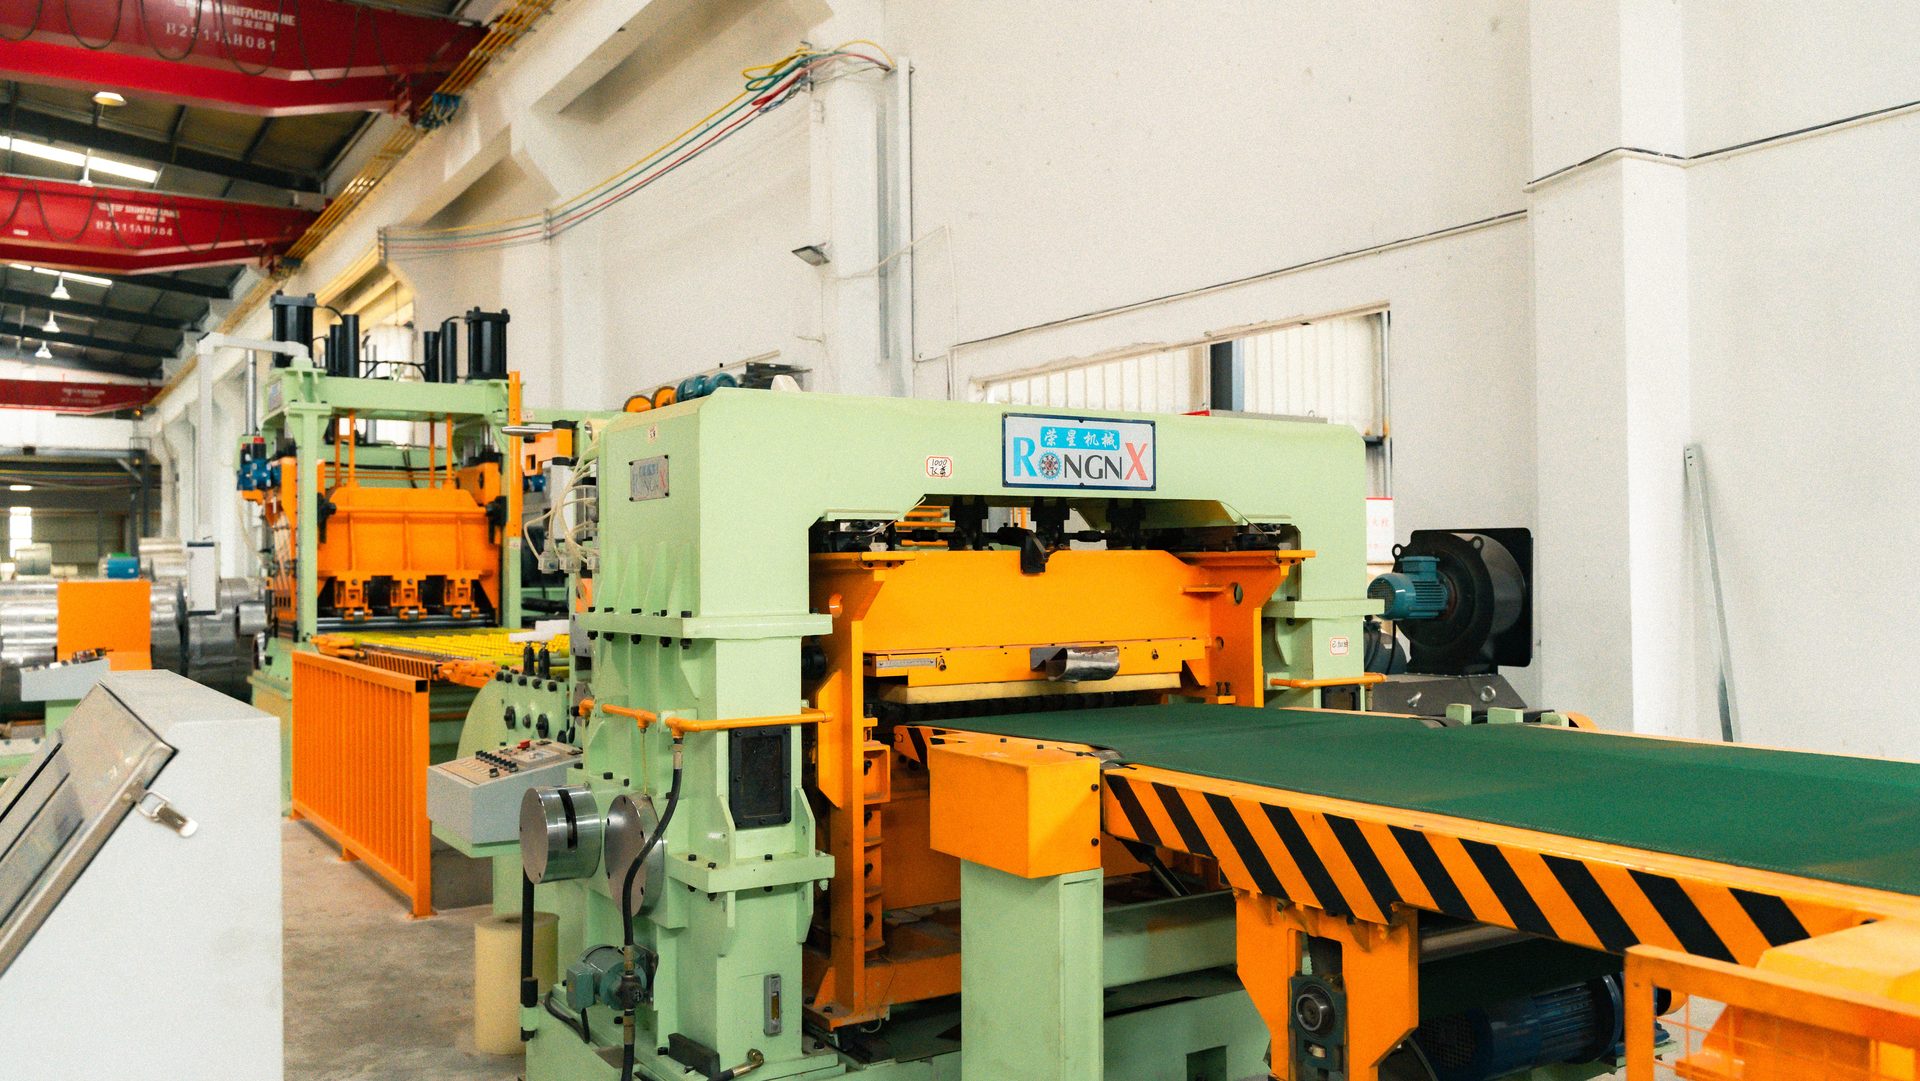
For another factory-test perspective, see the 1650mm Flying Shear preparation and delivery case. To create a project-specific protocol, send RONGXING the coil range, finished-sheet standard, sample plan and site conditions before the test date is fixed.